Catalytic Oxidizers
Industrial Catalytic Oxidizer Systems for Low-Temperature VOC & HAP Control
Stelter & Brinck catalytic oxidizers are designed for industrial air pollution control applications involving specified VOC- and HAP-laden process air streams.
Catalytic oxidizers operate at lower temperatures than many thermal oxidation systems and may be considered for applications where catalyst compatibility and energy use are important factors.
Our catalytic fume oxidizers are available with or without heat recovery and can be supplied as fully packaged, skid-mounted systems with prewired and prepiped assemblies.
Catalytic oxidizers may be considered for process air streams where catalyst-fouling agents or catalyst poisons are not present at levels that would interfere with operation.
Potential applications include:
- Aluminum and steel processing
- Bakeries and food processing
- Textile finishing
- Plastics and polymers
- Other industrial processes with specified VOC or HAP emissions

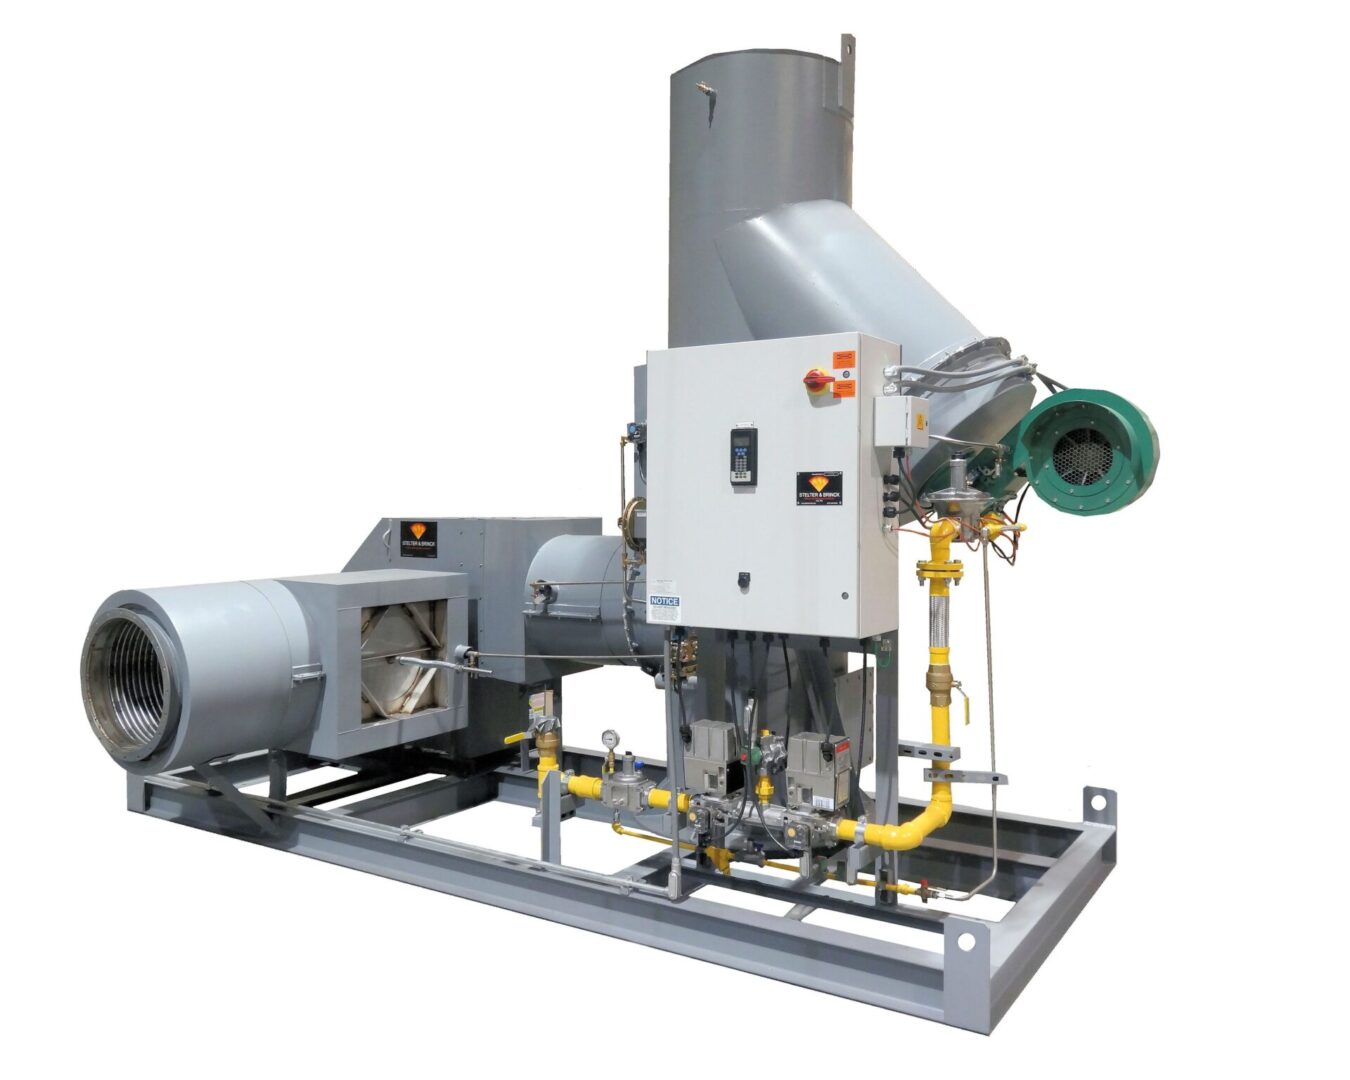
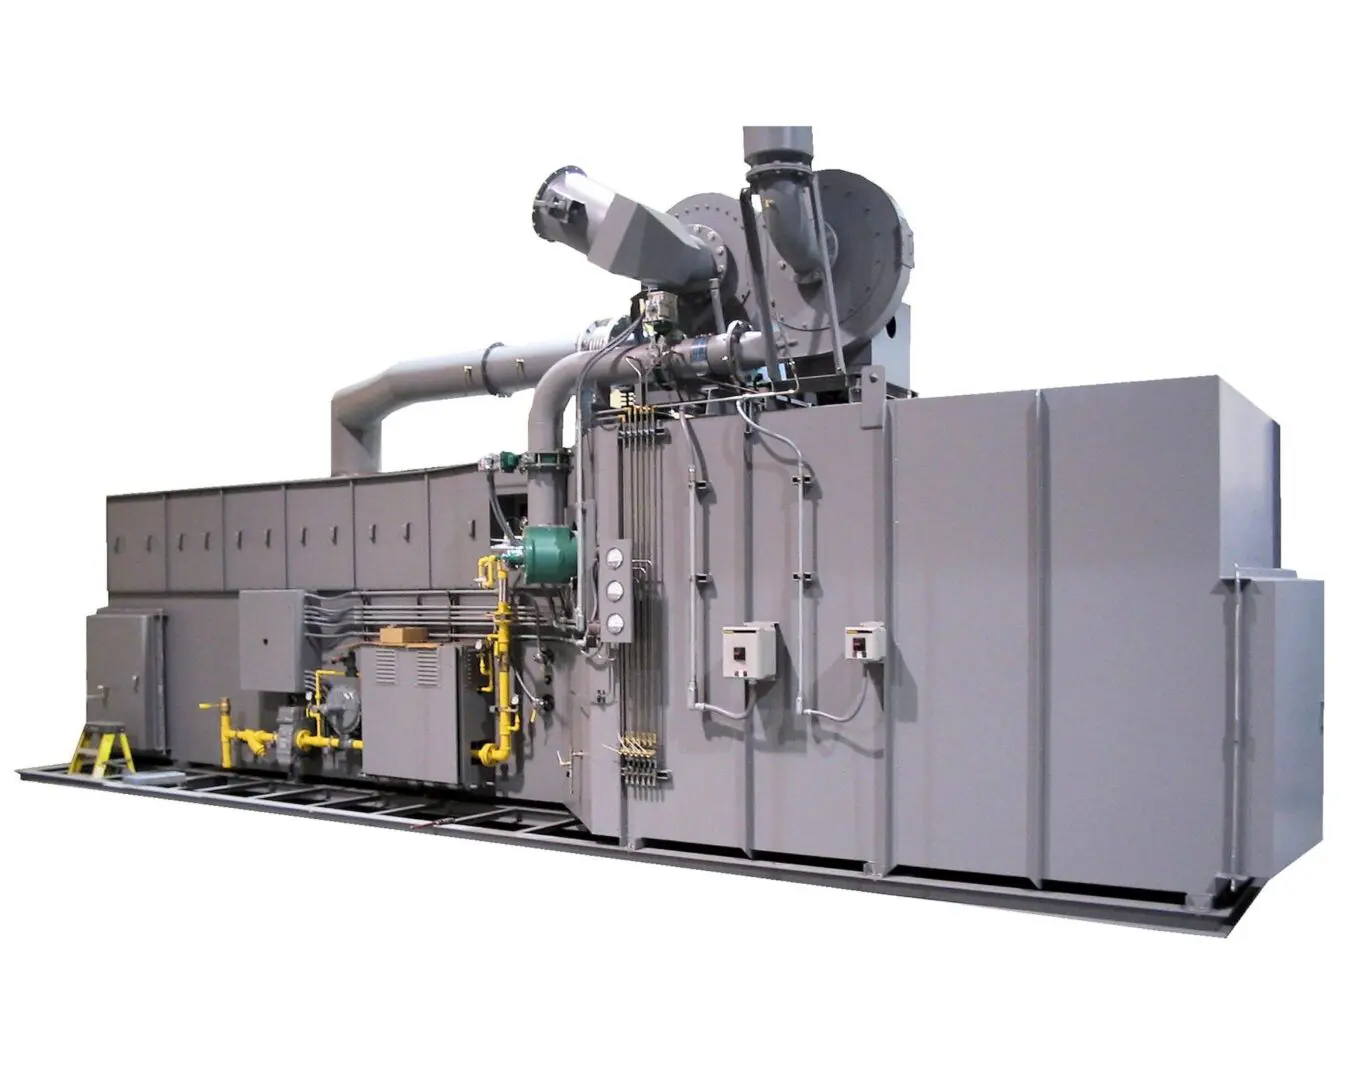
Installed Stelter & Brinck Oxidizer

Installed Catalytic Fume Oxidizer

Catalytic Oxidizer
FEATURES
S&B catalytic oxidizers are designed for straightforward installation, operation, and maintenance.
- Integrated Control Panel - Control panels can include annunciator, PID digital temperature control, FM-approved high-temperature limit, flame-safety relay, main power disconnect, and control transformer. UL 508A panels are available upon request.
- Remote Control Interface- PLC and DCS interface capabilities are available for integration with plant control systems.
- Application-Specific Configuration- Equipment can be configured based on customer-supplied process data, airflow requirements, contaminant characteristics, operating conditions, and specified project requirements.
- Applicable Construction Standards- Equipment and combustion components can be supplied to applicable FM, NFPA, GAP, CE, CSA, and other specified standards.
- Low-Emissions Options- Low-emissions combustion options are available for applicable applications.
- Factory Test-Firing & Combustion Tuning- Systems are test-fired and combustion-tuned prior to shipment to support efficient installation and start-up.
- Service & Maintenance- Ongoing service, maintenance, troubleshooting, repairs, upgrades, and parts support are available for S&B catalytic oxidizers and other combustion equipment.
S&B OXIDIZER BENEFITS:
Backed by more than 100 years of industrial combustion experience, Stelter & Brinck provides catalytic oxidizer systems for a variety of industrial emissions-control applications.
- Lower-Temperature Operation – catalytic oxidation can operate at lower temperatures than many thermal oxidation systems when the application is suitable.
- Packaged Systems – prewired and prepiped assemblies simplify installation and field connections.
- Integrated Controls – combustion and process-control components are incorporated into the packaged system.
- Heat Recovery Options – recuperative configurations can reclaim available heat from the treated exhaust stream.
- Heavy-Duty Construction – designed for demanding industrial environments.
- Application Flexibility – configurations are available based on specified process conditions.
- Service-Friendly Design – access is provided for routine inspection and catalyst maintenance.
- Factory Testing – systems are test-fired and combustion-tuned prior to shipment.
- Ongoing Support – S&B provides start-up, maintenance, troubleshooting, parts, and combustion service.
MODELS
CATALYTIC FUME OXIDIZER WITH HEAT RECOVERY (CFO-HX)
For suitable applications operating below 20% LEL, the CFO-HX combines catalytic oxidation with heat recovery to reclaim available heat from the process exhaust stream.
Catalytic oxidizers are generally suited for process air streams that are free of catalyst-fouling agents or poisons. Final suitability depends on the specific contaminant characteristics and operating conditions of the application.
The system operates within a specified temperature range, typically approximately 650°F–750°F, depending on application requirements and equipment configuration.
- Burner access door for maintenance
- Optional test platforms for in-plant testing and inspection
- Process fan with TEFC motor
- Optional CE ratings
- Emission inlet with purge-air tee damper
- Catalyst access door
- Prewired and prepiped construction
- Factory test-firing and combustion tuning
- FM, NFPA, or GAP (IRI) approved valve train options
- Shell-and-tube heat exchanger manufactured by S&B
- Heat exchanger configurations available based on specified application requirements
CATALYTIC FUME OXIDIZER WITHOUT HEAT RECOVERY – DIRECT (CFO)
For suitable process air streams that are free of catalyst-fouling compounds or poisons, the CFO provides low-temperature catalytic oxidation in a compact, packaged configuration.
Operating temperature is typically in the 650°F–750°F range, depending on the specified application and equipment configuration.
- Flow-control damper for process-air management
- Process fan with TEFC motor
- Purge-air damper and emission inlet assembly
- Skid-mounted packaged construction
- Prewired and prepiped assembly
- Factory test-fired prior to shipment
- FM, NFPA, or GAP (IRI) approved valve train options
- Optional CE ratings